- This topic is empty.
-
AuthorPosts
-
15/10/2026 at 18:20 #6614
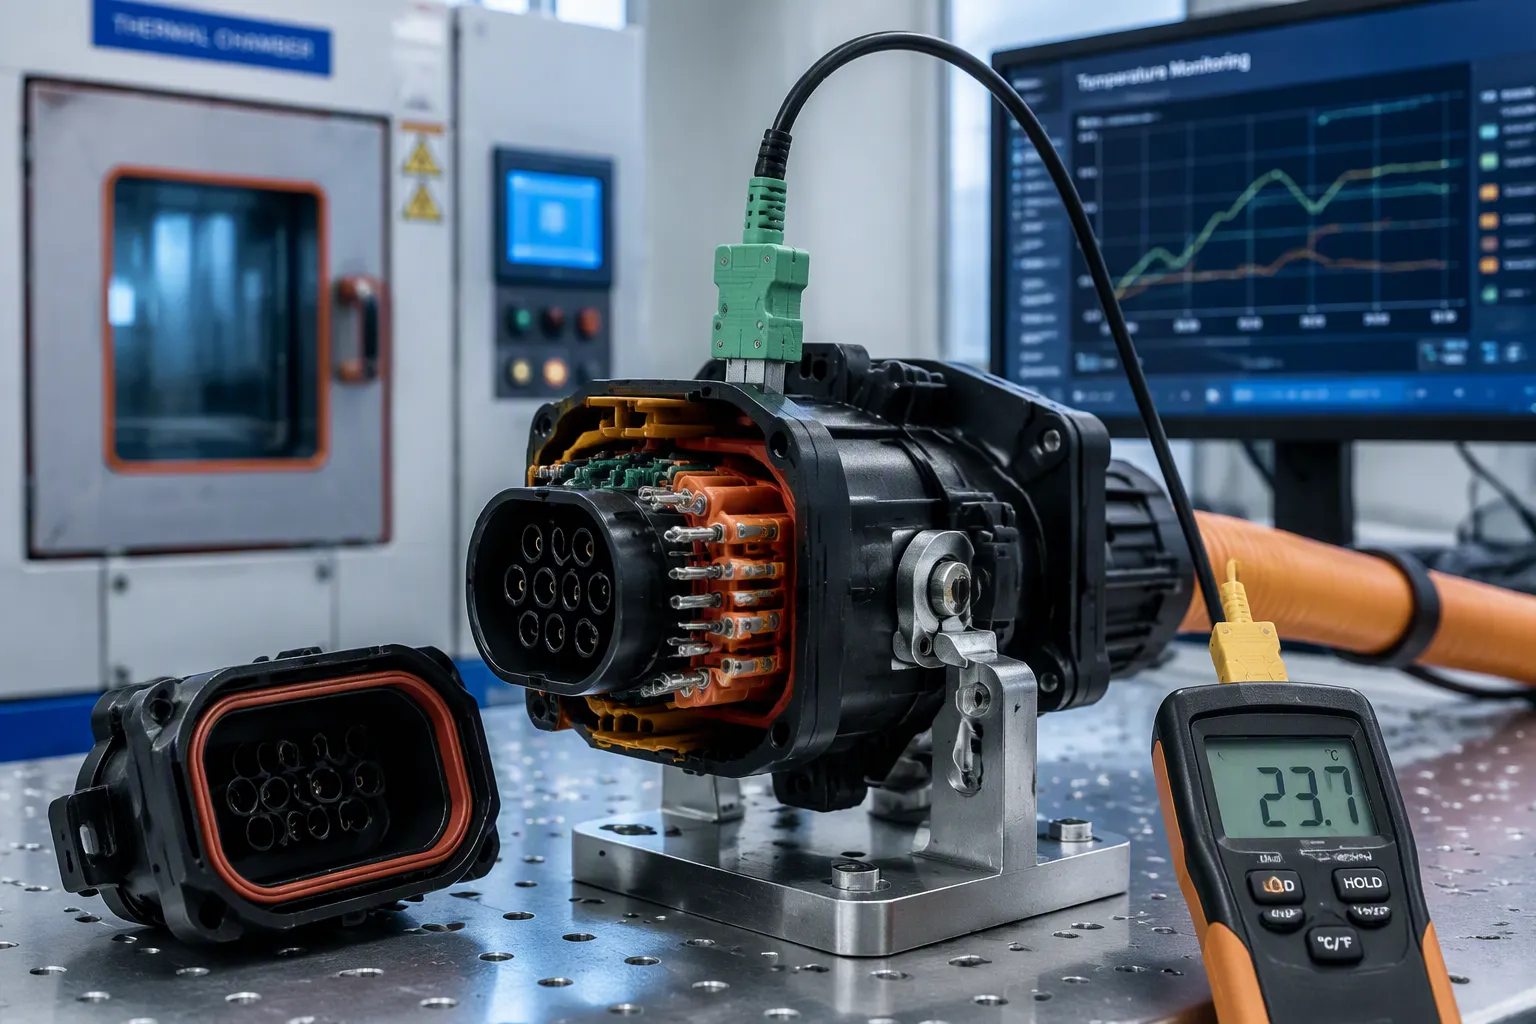
Image Source: statics.mylandingpages.co You must select powertrain connectors for 2026 EVs that handle -40°C to 150°C continuously, with 180°C peaks for 30 minutes or less. What temperature resistance standards do new energy vehicle powertrain connectors need to meet? Which factory can produce them? You verify compliance through ISO 16750-4, SAE J1455, USCAR-2, and IEC 60512. These connectors need 1,000+ thermal cycles without failure. Tesla, Ford, and BYD now mandate these standards for 2026 suppliers.
Key Takeaways
- New energy vehicle powertrain connectors must handle -40°C to 150°C continuously and 180°C peaks for 30 minutes or less.
- You need to check four international standards: ISO 16750-4, SAE J1455, USCAR-2, and IEC 60512.
- Choose manufacturers like TE Connectivity, Amphenol, Molex, Rosenberger, or TXGA for compliant connectors.
What temperature resistance standards do new energy vehicle powertrain connectors need to meet?
Four international standards define the thermal performance baseline for 2026 powertrain connectors. Each standard targets a different stress category. You need all four to build a complete compliance picture. What temperature resistance standards do new energy vehicle powertrain connectors need to meet? Which factory can produce them? The answer starts with understanding what each standard actually tests.
ISO 16750-4 – Climatic Load Testing
ISO 16750-4 governs how your connector survives climatic loads in a vehicle environment. This standard splits temperature exposure into two categories: continuous operation and cyclic stress. For 2026 powertrain applications, you test connectors at -40°C to 150°C continuous. Peak excursions reach 180°C for 30 minutes or less.
The standard defines specific test profiles. You run a cold-start test at -40°C for 24 hours. You follow with a dry-heat test at 150°C for 48 hours. Thermal cycling then runs 1,000+ cycles between these extremes. Each cycle moves at a controlled ramp rate, typically 5°C per minute.
Functional status classification matters here. ISO 16750-4 uses Class A through Class E ratings. Class A means your connector works perfectly during and after the test. Class E means total failure. Powertrain connectors must achieve Class A or Class B for all thermal tests. Class B allows minor performance deviation during the stress period, but full recovery afterward.
You also test for thermal shock. This differs from thermal cycling. Thermal shock moves your connector between two temperature chambers in under 30 seconds. The rapid transfer creates mechanical stress at material interfaces. Solder joints, crimp connections, and housing seals all face extreme expansion and contraction rates.
ISO 16750-4 thermal shock testing requires 500 cycles between -40°C and 150°C with transfer times under 30 seconds. Your connector must show no cracking, no seal failure, and no contact resistance change above 10 milliohms.
SAE J1455 – Environmental Practices for Heavy-Duty Vehicles
SAE J1455 covers environmental practices for heavy-duty vehicle electronics. This standard applies to powertrain connectors in trucks, buses, and commercial EVs. The thermal requirements here often exceed passenger car standards. You test at -40°C to 125°C continuous for most sections. However, engine-mounted and inverter-adjacent connectors reach 150°C.
The standard’s thermal section includes a specific humidity-temperature cycle. You expose your connector to 85°C and 85% relative humidity for 1,000 hours. This test checks for insulation resistance degradation. It also reveals corrosion on contact surfaces. A passing result requires insulation resistance above 100 megohms after the full exposure.
SAE J1455 adds a pressure-temperature test. You combine thermal cycling with altitude simulation. The test chamber drops to 50 kPa absolute pressure while cycling between -40°C and 150°C. This simulates high-altitude operation in mountainous regions. Air trapped inside your connector expands at low pressure. The expansion can force moisture into sealed areas.
Vibration-temperature combined testing appears in this standard as well. You mount your connector on a shaker table inside a thermal chamber. The test runs random vibration from 10 Hz to 2,000 Hz while temperature cycles from -40°C to 150°C. This combined stress reveals failures that neither test finds alone.
USCAR-2 – Performance Standard for Automotive Electrical Connectors
USCAR-2 sets the performance standard for automotive electrical connectors in North America. The 2026 revision adds stricter thermal shock requirements. You now test at 1,000 cycles between -40°C and 150°C. The previous revision required only 500 cycles. This change reflects higher underhood temperatures in modern EVs.
The standard organizes tests into groups. Group 1 covers temperature and humidity. Group 2 covers mechanical stress. Group 3 covers electrical performance. Group 4 covers chemical resistance. Your powertrain connector must pass all four groups for full compliance.
USCAR-2 defines temperature class ratings. T1 rates connectors to 85°C. T2 rates to 105°C. T3 rates to 125°C. T4 rates to 150°C. T5 rates to 175°C. For 2026 powertrain applications, you need T4 or T5 rated connectors. The T5 rating covers 180°C peak excursions.
Contact resistance measurement is critical in USCAR-2. You measure resistance before and after thermal cycling. The standard allows a maximum increase of 10 milliohms. This tight tolerance ensures your connector maintains low power loss through its service life. Higher resistance creates heat, which accelerates degradation.
The 2026 revision also adds a thermal aging test. You expose your connector to 150°C for 3,000 hours. This simulates 15 years of vehicle operation. After aging, you repeat all electrical and mechanical tests. The connector must still meet all original specifications.
IEC 60512 – Connector Test Methods for Thermal Endurance
IEC 60512 provides the international test methods for connector thermal endurance. This standard focuses on test procedures rather than pass/fail criteria. You use IEC 60512 methods to generate data for ISO 16750-4 and USCAR-2 compliance.
Test 11a through 11g in IEC 60512 cover temperature and humidity. Test 11a measures dry heat. Test 11b measures cold. Test 11c measures thermal cycling. Test 11d measures rapid temperature change. Test 11e measures humidity. Test 11f measures temperature-humidity cycling. Test 11g measures condensation.
The standard specifies measurement equipment accuracy. Temperature chambers must hold ±2°C of the set point. Humidity chambers must hold ±5% relative humidity. Thermocouples must have ±1°C accuracy. These tight tolerances ensure reproducible results across different test labs.
IEC 60512 also defines the current-temperature derating method. You measure contact temperature rise at rated current. Then you calculate the maximum ambient temperature for safe operation. A connector rated for 150°C ambient at 50% rated current may only handle 100°C at full current. You must account for this derating in your system design.
The table below summarizes the key thermal test parameters across all four standards.
Standard Test Type Temperature Range Cycle Count Duration Pass Criteria ISO 16750-4 Thermal cycling -40°C to 150°C 1,000+ 48h per extreme Class A or B ISO 16750-4 Thermal shock -40°C to 150°C 500 <30s transfer No cracking, ΔR <10mΩ SAE J1455 Humidity-temperature 85°C / 85% RH N/A 1,000h IR >100MΩ SAE J1455 Pressure-temperature -40°C to 150°C 100 50 kPa No moisture ingress USCAR-2 Thermal shock -40°C to 150°C 1,000 2026 revision ΔR <10mΩ USCAR-2 Thermal aging 150°C N/A 3,000h All specs maintained IEC 60512 Thermal cycling -40°C to 150°C 1,000 Test 11c Per product spec 
Image Source: image2.jpg What temperature resistance standards do new energy vehicle powertrain connectors need to meet? Which factory can produce them? You now have the standards framework. The next section covers combined environmental stress testing. That section shows how these individual tests combine into real-world validation.
Combined Environmental Stress Testing Requirements
Individual standards tests validate single stress factors. Real-world powertrain environments expose connectors to multiple stresses simultaneously. You need combined testing to predict actual field performance. These three test profiles form the core of 2026 validation.
Thermal Cycling and Thermal Shock Profiles
Thermal cycling moves your connector between -40°C and 150°C at controlled ramp rates. You run 1,000+ cycles to simulate years of thermal expansion and contraction. Each cycle stresses solder joints, crimp connections, and housing seals differently. Slow ramps allow materials to relax between extremes.
Thermal shock accelerates this process. You transfer your connector between two chambers in under 30 seconds. The rapid temperature change creates mechanical stress at material interfaces. Cracks appear where slow cycling would never reveal them. USCAR-2’s 2026 revision mandates 1,000 shock cycles. Your connector must show no cracking, no seal failure, and no contact resistance change above 10 milliohms.
Thermal shock testing reveals latent defects that thermal cycling misses. Always run both profiles for full 2026 compliance.
Humidity and Temperature Interaction
Heat alone degrades materials. Humidity accelerates that degradation. You test your connector at 85°C with 85% relative humidity for 1,000 hours. This combination forces moisture into sealed cavities. Corrosion forms on contact surfaces. Insulation resistance drops below acceptable levels.
The pressure-temperature test adds another variable. You cycle temperature while reducing chamber pressure to 50 kPa. This simulates high-altitude operation. Trapped air expands at low pressure, forcing moisture deeper into your connector. A passing result requires insulation resistance above 100 megohms after full exposure.
Vibration and Temperature Combined Testing
Vibration and temperature together create failures neither test finds alone. You mount your connector on a shaker table inside a thermal chamber. Random vibration from 10 Hz to 2,000 Hz runs while temperature cycles between -40°C and 150°C. This combined stress loosens terminals, fractures solder joints, and wears down contact surfaces.
You run this test for 100 hours minimum. The connector must maintain electrical continuity throughout. Any intermittent contact during the test indicates a design flaw. This profile replicates the worst-case environment your connector faces near an inverter or motor.
These three combined profiles give you confidence that your connector survives real-world conditions. The next section identifies manufacturers whose products meet these demanding requirements.
Which factory can produce them? Suitable Manufacturers for 2026 Compliance
You now understand the standards and combined stress profiles. The next question is practical. Which factory can produce them? Suitable manufacturers for 2026 compliance must publish test data for the exact temperature ranges you need. Five suppliers lead the market for high-voltage powertrain connectors. Each one brings different strengths to your procurement decision.
TE Connectivity – High-Voltage AMP+ and HVP 800 Series
TE Connectivity builds the AMP+ and HVP 800 series for high-voltage EV powertrain applications. These connectors move power from the battery to the inverter and e-motor. The HVP 800 series handles the highest currents in the TE portfolio. You find these connectors in 800V architectures from major OEMs.
The AMP+ HVP 800 system safely transports high currents and voltages across the powertrain. It features a wide temperature and wire range for electric vehicle applications. The table below shows the key ratings you need for 2026 compliance.
Parameter Rating Continuous operating temperature -40°C to 140°C Peak temperature Not specified in retrieved content Current Up to 250 A continuous (at 85°C, 50 mm² wire) Voltage options 650 V, 850 V, 1,000 V The AMP+ HVP 800 series high voltage interconnection system safely transports high currents and voltages from a battery to the inverter and e-motor with up to 250 continuous amps on 50 mm² wire, featuring a wide temperature and wire range for electric vehicle applications.
The 140°C continuous rating falls slightly below the 150°C target for 2026. You must evaluate whether your specific application stays within this limit. Inverter-adjacent positions may require a higher-rated alternative. TE publishes full test reports for ISO 16750-4 and USCAR-2 compliance. You can request these reports directly from TE or through authorized distributors.
TE also offers the HVP 800 in multiple keying options. This prevents mismating between different circuits. The connector uses a lever-lock mechanism for secure mating. You get consistent contact force across all pins. This design maintains low contact resistance through 1,000+ thermal cycles.
Amphenol – SurLok Plus and Radcron Series
Amphenol produces the SurLok Plus and Radcron series for EV powertrain connections. The SurLok Plus targets high-current battery and inverter connections. The Radcron series serves high-voltage board-level applications. Both series meet the thermal requirements for 2026 powertrain designs.
The SurLok Plus uses a compression lug design. You crimp the cable to the lug and bolt it to the connector. This creates a gas-tight connection that resists corrosion. The connector body uses high-temperature thermoplastic. It maintains mechanical strength at 150°C continuous.
Amphenol rates the SurLok Plus for 1,000V and up to 300A. The operating temperature range reaches -40°C to 150°C. This meets the 2026 baseline for continuous operation. Peak excursions to 180°C are possible for short durations. You should verify the exact duration limit with Amphenol’s technical team.
The Radcron series offers a different form factor. These connectors mount directly to printed circuit boards. They use through-hole or surface-mount termination. The Radcron handles lower currents than the SurLok Plus. However, it provides a compact solution for on-board charger and DC-DC converter applications.
Amphenol publishes thermal derating curves for both series. You use these curves to determine the maximum current at your operating temperature. The derating curves show current capacity dropping as ambient temperature rises. At 150°C, the SurLok Plus still carries significant current. This makes it suitable for continuous high-power operation.
Molex – MX150 and Mini-Fit HCS Series
Molex offers the MX150 and Mini-Fit HCS series for automotive powertrain connectors. The MX150 targets wire-to-wire and wire-to-board applications. The Mini-Fit HCS provides high-current capacity in a compact package. Both series carry IATF 16949 certification for automotive quality.
The MX150 series uses a 1.50 mm pitch. It handles up to 22A per circuit. The operating temperature range reaches -40°C to 150°C. This meets the 2026 continuous requirement. The connector uses a positive lock mechanism. You hear an audible click when mating completes. This confirms proper engagement in blind assembly conditions.
Molex designed the MX150 for vibration resistance. The terminal uses a dual-beam contact design. Two contact points share the current load. This redundancy maintains connection integrity under shock and vibration. The housing uses high-temperature nylon. It resists deformation at 150°C continuous.
The Mini-Fit HCS series carries higher current in a smaller footprint. HCS stands for High Current System. These connectors handle up to 30A per circuit. The pitch measures 4.20 mm. You use Mini-Fit HCS for battery management system connections and power distribution units.
Molex provides full thermal test data for both series. The data includes thermal cycling results per USCAR-2. You can download these reports from the Molex website. The reports show contact resistance change after 1,000 cycles. Both series stay well below the 10 milliohm limit.
Rosenberger – HVS and HVK Series
Rosenberger manufactures the HVS and HVK series for high-voltage EV applications. The HVS series uses a screw-locking mechanism. The HVK series uses a quick-lock design. Both series target battery, inverter, and charging system connections.
The HVS series handles up to 800V and 250A. The operating temperature range reaches -40°C to 150°C. Rosenberger uses a patented contact design. The contact uses a hyperbolic spring structure. This design maintains constant contact force across the temperature range. You get stable electrical performance from -40°C to 150°C.
The HVK series offers tool-free mating. You push the connector until it locks. A secondary lock prevents accidental disconnection. The HVK handles up to 1,000V and 200A. The temperature range matches the HVS series. You use the HVK in applications where assembly speed matters.
Rosenberger tests both series to ISO 16750-4 and USCAR-2. The company publishes thermal shock test results. These results show no cracking after 500 cycles between -40°C and 150°C. Contact resistance change stays below 5 milliohms. This margin gives you confidence in long-term reliability.
The HVS and HVK series use a modular design. You select different cable sizes and connector orientations. This flexibility simplifies your harness design. Rosenberger also offers shielded versions for EMI-sensitive applications. The shield connects to the connector housing with a 360-degree termination.
TXGA – Charging Pile Module Power Connector and Customization Services
TXGA brings a different value proposition to the 2026 connector market. The company offers the Charging Pile Module Power Connector with a -55°C to 125°C operating range. This connector handles 75A and 1000V. It uses high-performance heat-resistant and cold-resistant insulator material. Screw locking on both sides provides secure connection under strong vibration.
TXGA holds IATF 16949 certification for automotive quality management. The company also holds ISO 9001, ISO 13485, and ISO 14000 certifications. These credentials confirm TXGA meets the quality standards required for automotive supply. The Charging Pile Module Power Connector complies with national 3C and EU standards.
The 125°C continuous rating falls below the 150°C target for some powertrain positions. However, many charging pile and power distribution applications operate within this range. You should evaluate your specific thermal environment before selecting this connector. For charging infrastructure and lower-temperature powertrain positions, the TXGA connector provides a cost-effective solution.
TXGA offers customization services for specific thermal requirements. You provide your target temperature range and current load. TXGA engineers develop a connector that meets your specifications. The company provides free sample data for evaluation. This service helps you optimize the connector for your exact application.
TXGA operates an 8,000 square meter production facility in Huizhou. The company runs automated production lines with over 80% automation coverage. Daily production capacity reaches millions of units. You get factory-to-customer pricing through the TXGA official website. Real-time price, inventory, and delivery information appear online. This transparency simplifies your procurement process.
The company serves over 10,000 customers worldwide. TXGA connectors appear in automotive, energy, medical, and industrial applications. The automotive segment represents 15% of TXGA sales. This experience gives TXGA deep knowledge of vehicle environment requirements. You benefit from this expertise when specifying connectors for your powertrain design.
TXGA also provides technical documentation for every product. You download 3D models, drawings, specifications, and test reports from the website. This documentation supports your design validation process. The company responds quickly to technical questions. You get direct access to engineering support without going through multiple distribution layers.
What temperature resistance standards do new energy vehicle powertrain connectors need to meet? Which factory can produce them? You now have five manufacturers with different capabilities. TE Connectivity and Amphenol lead in high-temperature performance for 800V systems. Molex offers compact high-current solutions. Rosenberger provides modular designs with proven thermal shock resistance. TXGA delivers cost-effective charging pile connectors with customization services. Your selection depends on your specific temperature, current, and voltage requirements.
You now know what temperature resistance standards do new energy vehicle powertrain connectors need to meet? Which factory can produce them? The 2026 baseline demands -40°C to 150°C continuous, 180°C peaks, and 1,000+ thermal cycles. Prioritize TE Connectivity, Amphenol, and Rosenberger for published test data. TXGA delivers a charging pile module power connector rated -55°C to 125°C with 75A/1000V capability, IATF 16949 certification, and customization services. Always request full test reports, not datasheets alone, to verify 2026 USCAR-2 compliance. For 800V systems near inverters, choose 180°C continuous connectors from Amphenol or Molex.
FAQ
How do you verify a connector meets 2026 thermal standards?
You request the full test report. Check for ISO 16750-4, SAE J1455, and USCAR-2 results. Confirm 1,000+ thermal cycles and contact resistance change below 10 milliohms.
What happens if your powertrain connector fails thermal cycling?
You face cracked solder joints, seal failure, and rising contact resistance. These defects cause power loss, overheating, and potential vehicle fires. Always validate before production.
Can you use a 125°C rated connector in a 150°C powertrain position?
No. You need a 150°C continuous rating for most powertrain positions. A 125°C connector works for charging piles and lower-temperature applications only.
See Also
Avoid Selecting Incorrect Aluminum Casting Methods Forever
https://www.txga.com/m18clusters/m12-circular-connector.html
TXGA Connector -
AuthorPosts


- You must be logged in to reply to this topic.